 how-to
Quality Assurance for Business Print Orders: 2026 Guide
Table of Contents
- What Quality Assurance for Business Print Orders Actually Involves
- Pre-Press File Preparation Best Practices That Prevent Rework
- Commercial Printing Color Consistency Standards You Should Require
- Your Print Quality Control Checklist for Every Order
- Common Print Defects and How to Prevent Them
- What to Look for in a Print Partner
- Frequently Asked Questions
Last Updated: September 10, 2026
What Quality Assurance for Business Print Orders Actually Involves
Quality assurance for business print orders is the set of checks and standards applied before, during, and after production to ensure every printed piece matches your brand specifications. At American Printing Services, LLC, we treat it as a system, not a final inspection.
The core idea is simple: prevention beats correction. A QA program covers file preparation, proof approval, press monitoring, and post-production inspection. Each stage catches what the previous one missed.
Quality Control vs. Quality Assurance in Printing
Quality control is reactive. It inspects finished output and flags defects. Quality assurance is proactive. It builds processes, standards, and checkpoints into the production workflow so defects are less likely to occur in the first place.
Most print problems trace back to a missing preventive step, not a careless press operator. That's why the strongest print programs invest in pre-press discipline as much as press monitoring.
Pre-Press File Preparation Best Practices That Prevent Rework
The cheapest place to fix a print defect is in the digital file. Pre-press file preparation is where rework and waste reduction start, because a file error caught on screen costs nothing to correct, while the same error caught on press wastes substrate, ink, and time. A single wasted press make-ready on a 5,000-sheet offset run can consume hundreds of sheets before color is approved, sheets that go straight to recycling.
A common mistake is sending a file straight from a design tool without checking resolution, color mode, or bleed. Print-ready files need specific technical attributes, and each one exists for a mechanical reason:
- Resolution. Offset and digital presses reproduce raster images as halftone dots. At 300 DPI at 100% print size, the dots resolve below the eye's threshold at normal reading distance (printwiki.org). Drop to 150 DPI and the dot grid becomes visible as pixelation on glossy stock.
- Color mode. A press lays down cyan, magenta, yellow, and black ink. RGB values are device-dependent screen colors that must be converted, and the conversion is not lossless. Supplying CMYK with an embedded profile hands the printer a known starting point instead of a guess.
- Bleed. Trimming is a mechanical cut with normal variance of roughly 1/16 inch. Bleed of at least 0.125 inches beyond the trim line gives the cutter room to drift without leaving a white sliver at the edge.
- Safe zone. The same trim variance can clip content that sits too close to the edge. Keeping critical text and logos at least 0.125 inches inside the trim line protects them.
- Fonts. A font that isn't embedded or converted to outlines gets substituted at the RIP, and substitution changes letter spacing, line breaks, and sometimes the entire layout.
- Vector vs. raster. Logos and line art stay sharp at any size only as vector. Rasterizing a logo locks it to one resolution.
- File format. PDF/X-1a and PDF/X-4 are ISO-standardized exchange formats that embed fonts, flatten or preserve transparency predictably, and lock color intent. A native design file does none of that reliably.
Two failure modes deserve special attention because they survive a casual visual check:
Rich black vs. flat black. Large black areas built from 100% K alone can print thin and gray. A rich black built from roughly 60C/40M/40Y/100K reads deeper, but the same build on small body text causes misregistration halos. The rule most shops follow: rich black for large solids, 100% K for text.
Overprint and knockout. Overprint settings determine whether an object knocks out the ink beneath it or prints on top. Set wrong, white text on a dark background can disappear or pick up a ghosted edge. Pre-flight software flags these, but only if someone reads the report.
Digital File Pre-Flighting Checklist
Run every file through this checklist before it reaches the printer. This is the same sequence a prepress operator runs, in the same order:
- Resolution: 300 DPI minimum for raster images at 100% print size
- Color mode: CMYK for print, with an embedded color profile
- Rich black: 60C/40M/40Y/100K for large solids, 100% K for body text
- Overprint: reviewed and set intentionally, not left at default
- Bleed: at least 0.125 inches beyond the trim line
- Trim and safe zones: critical text and logos at least 0.125 inches inside the trim
- Fonts: embedded or converted to outlines
- Vector graphics: logos and line art kept as vector, not rasterized
- File format: PDF/X-1a or PDF/X-4 preferred for commercial printing
- Page count and dimensions: match the print specification exactly
- Spot colors: Pantone values named correctly and mapped to the right plates
A pre-flight report is only useful if someone acts on it. The most common pattern in rework is a flagged file that ships anyway because the deadline was tight. Building a hard stop into the workflow, no file advances to plate or press until the pre-flight report is clean or the exception is signed off, is what turns the checklist from a suggestion into a control.
Commercial Printing Color Consistency Standards You Should Require
Color consistency across batches is the single most common complaint businesses raise about print vendors. A brand's identity depends on the same red looking like the same red on every brochure, label, and banner, whether printed digitally or offset. The reason color drifts is mechanical: ink film thickness, press temperature, substrate absorbency, and dot gain all vary, and each one shifts the final appearance.
Industry standards exist to pin those variables down. Two matter most for commercial work:
ISO 12647 is the international family of standards for process control in printing. It defines target values for solid ink density, dot gain (also called tonal value increase), gray balance, and registration tolerance across different printing processes, offset sheetfed, offset heatset web, gravure, and more. When a shop says it prints "to ISO 12647-2," it means sheetfed offset work is measured against published targets rather than a subjective eyeball call.
GRACoL (General Requirements for Applications in Commercial Offset Lithography) is the North American characterization data set maintained under IDEAlliance. GRACoL 2013 is the current widely referenced version, and it specifies the ink, paper, and measurement conditions under which a press run is considered on-standard. A shop running to GRACoL is measuring press sheets with a spectrophotometer and comparing them to a known reference, not just looking at them.
What this means practically: ask your print partner three questions.
-
What standard do you print to, and on what substrate? ISO 12647 and GRACoL targets differ by paper type. A coated sheet and an uncoated sheet have different dot gain behavior, and a shop that applies one target to both will miss on one of them.
-
How do you measure? A spectrophotometer reading a control strip is the standard method. Visual comparison under a viewing booth is a supplement, not a substitute.
-
What is your tolerance? Most shops hold average color difference (Delta E) within about 2 to 3 units for brand-critical work, with individual patches sometimes allowed to drift further. Ask what number they commit to.
Holding Color Across Runs and Locations
A single approved proof is not a color management system. Color drifts over a long press run as ink and water balance shifts, and it drifts between facilities when presses, chemistry, and operators differ. Three controls close that gap:
- Control strips. A color bar printed in the trim area of every sheet lets the operator read density and dot gain throughout the run, not just at the start.
- Batch testing across facilities. For multi-location orders, print a test sheet at each facility against the same reference and compare measurements before releasing the full run. This catches press-to-press variation before it reaches the customer.
- Reference proofs. Keep a physical approved proof on hand at each production site. Digital reference files drift as monitors and software change; a physical proof does not.
Digital and offset presses also reproduce color differently. Digital toner sits on the surface of the sheet; offset ink absorbs into it. The same CMYK values can produce visibly different results across the two processes. If an order spans both, ask for a proof from each process before committing.
Your Print Quality Control Checklist for Every Order
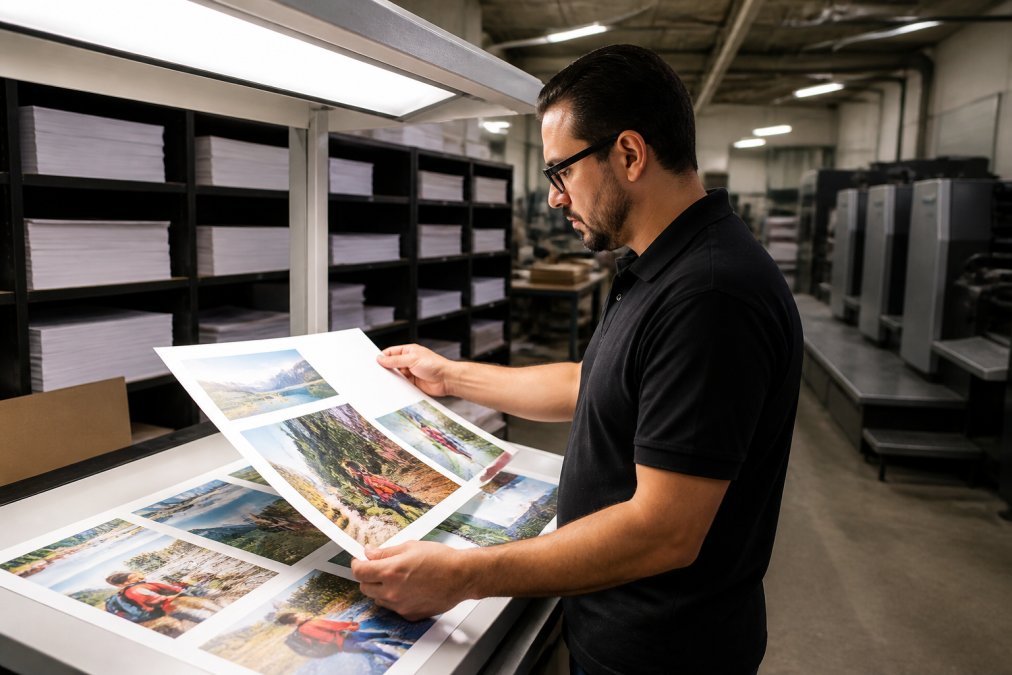
A print quality control checklist turns a vague promise of "good quality" into a repeatable process. Use the same checklist for every order, whether it's a single run of business forms or a nationwide rollout of branded collateral.
Before signing off on any print order, verify:
| Checkpoint | What to Inspect | Why It Matters |
|---|---|---|
| Color accuracy | Match against approved proof under D50 lighting | Protects brand identity across batches |
| Registration | Alignment of CMYK layers, no ghosting | Sharp text and images, no blur |
| Ink density | Even coverage, no mottling or streaking | Consistent appearance across the run |
| Substrate quality | No warping, tears, or coating defects | Affects durability and finish |
| Trim and bleed | Clean cuts, no content clipped | Prevents wasted reprints |
| Finishing | Correct folds, binding, and coatings | Delivers the intended finished product |
Post-Production Inspection Techniques
Post-production inspection catches defects the press check missed. Pull sample sheets from throughout the run, not just the top of the stack, and inspect them under consistent lighting. Compare against the approved proof. Check folds, bindings, and coatings on finished pieces, not just flat sheets.
For large orders, pull samples from the first, middle, and last portions of the run. Color and registration can drift over a long press run, and inspecting only the first sheets hides that drift.
Common Print Defects and How to Prevent Them
Most print defects fall into a handful of recurring categories, and nearly all of them are preventable with the right upstream controls. Here's how to handle the most common ones.
- Color shift between batches: Prevented by color profiles, proof approval, and batch testing.
- Misregistration (color layers out of alignment): Prevented by press calibration and registration checks.
- Ink streaking or mottling: Prevented by ink density monitoring and substrate checks.
- Blurry or pixelated images: Prevented by enforcing DPI minimums in pre-press.
- Content clipped at the trim: Prevented by correct bleed and safe-zone setup.
- Inconsistent finishing: Prevented by inspecting folded and bound samples, not just flat sheets.
Skilled operators matter here. Automated inspection catches a lot, but experienced press operators notice subtle drift before it becomes a defect. Ask any print partner how they train and retain their production staff.
What to Look for in a Print Partner
The right print partner builds quality assurance into their process rather than promising it after the fact. When vetting a commercial printing vendor, ask about their pre-press review process, their color management standards, and how they handle reprints when something goes wrong.
Look for documented standard operating procedures, a clear proof approval workflow, and a track record with multi-location or high-volume orders. A partner with a broad production network can also maintain consistent supply when demand spikes, which matters if you're coordinating collateral across multiple sites.
American Printing Services, LLC brings over 20 years of industry experience and a network of more than 2,500 production facilities across the United States, Canada, and Mexico. That network supports consistent supply and fast turnaround for businesses that need dependable delivery on every order.
Frequently Asked Questions
What is the difference between quality control and quality assurance in printing?
Quality control catches defects on a specific job: checking ink density, registration, and trim on the sheets coming off the press. Quality assurance is the system that prevents those defects from happening in the first place, covering file pre-flighting, proof approval, standard operating procedures, and operator training. A shop can pass QC on one order and still fail QA overall if the same color variation or misregistration keeps recurring across jobs. Strong print quality assurance programs build checks into every stage, from file receipt through post-production inspection.
What file specifications are required to ensure high-quality print results?
Supply print-ready PDFs with all fonts embedded and images at 300 DPI at final size. Convert RGB artwork to CMYK, include 0.125 inches of bleed on every side, and keep critical text and logos at least 0.125 inches inside the trim line. Vector graphics should stay vector rather than being flattened into raster images. Following pre-press file preparation best practices like these prevents the most common causes of rework: missing fonts, low-resolution images, and artwork that gets clipped at the trim.
How do you verify color consistency across large print orders?
Ask your printer to run the job to a defined standard such as GRACoL or SWOP, measured with a spectrophotometer rather than judged by eye. Request a press proof or a contract proof for approval before the full run, and have the shop pull and measure sheets at the start, middle, and end of the run. For orders spanning multiple batches or locations, keep the approved proof on file and require every reprint to match it. This is how commercial printing color consistency standards keep brand colors identical across batches.
How can businesses minimize print defects in high-volume orders?
Build quality checks into the production workflow instead of inspecting only at the end. Pre-flight every file, get written proof approval, confirm substrate quality and ink density targets before the run starts, and pull inspection sheets at regular intervals. Track defect types and rework rates so recurring problems get fixed at the source. A documented print quality control checklist, applied to every order regardless of size, reduces waste and protects turnaround time on high-volume runs.
Consistent branded materials depend on a print partner who treats quality assurance as a system, not an afterthought. American Printing Services, LLC combines over two decades of experience, a nationwide production network, and comprehensive service covering everything from business forms to branded merchandise to keep your materials precise and on time. Get started with American Printing Services, LLC and give every print order the quality control it deserves.